Key Specifications at a Glance Material Grade: Inconel® X-750 (UNS N07750 / W.Nr. 2.4669) Density: 8.28 g/cm³ Melting Range: 1393 – 1427°C (2540 – 2600°F) Key Strengthening Mechanism: Precipitation-hardened (γ' phase) Available Forms: Bar, Sheet, Strip, Wire, Tube, Forging, Ring, Disc, Coil Certifications: AS 9120B, ISO 9001:2015 (ZYTC Alloy)
Quantity :
add to cart
Contact Now
Inconel® X-750 is a Nickel-Chromium alloy made precipitation hardenable by additions of Aluminium and Titanium, having creep-rupture strength at high temperatures to about 700°C (1290°F).
Alloy X-750 is widely used in aerospace engines, gas turbines, nuclear reactors, rocket engines, and high-temperature spring applications, where reliability under extreme stress and temperature conditions is non-negotiable.
As a professional China nickel alloy supplier, ZYTC Alloy provides standardized Inconel® X-750 products including bars, plates, sheets, wires, forgings and custom machined parts. All materials comply with international industry standards, with complete heat treatment processes and full MTR certification, supporting global high-end equipment manufacturing and engineering procurement projects.
Why Choose ZYTC Alloy Inconel X-750 Superalloy?
Quality Assurance
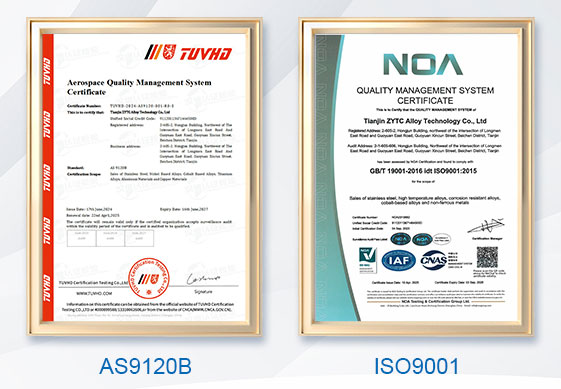
We strictly adhere to ASTM B637,AMS 5598,AMS 5542,AMS 5582,AMS 5667 and AMS 5670 standards. Each batch undergoes chemical composition analysis, tensile testing, and hardness verification, with complete inspection reports provided to ensure full material traceability. Our AS 9120B and ISO 9001:2015 certifications guarantee supply chain quality management.
Delivery Capability
We maintain stock for standard sizes across multiple forms (bar, sheet, wire, coil) and support custom length, diameter, and tolerance requirements, with a typical lead time of 4-6 weeks.
Technical Support
Our engineering team provides material selection guidance, heat treatment recommendations, and processing consultation to help you optimize product performance and cost.
Chemical Composition
Element
Min
Max
Carbon
--
0.08
Manganese
--
0.30
Silicon
--
0.50
Sulfur
--
0.01
Nickel + Cobalt
70.0 min
Chromium
14.0
17.0
Iron
5.00
9.00
Aluminum
0.40
1.00
Titanium
2.25
2.70
Copper
--
0.50
Cb + Ta
0.70
1.20
Physical Properties
Property
Value
Density
8.28 g/cm³
Melting Range
1393 – 1427°C
Thermal Conductivity
Temperature
Btu-in/ft²-hr-°F
W/m-K
°F
°C
300
149
117
16.9
600
316
142
20.5
1000
538
184
26.5
1200
649
199
28.7
1400
760
218
31.4
1600
871
245
35.3
Electrical Resistivity
Condition
ohm-cir mil/ftAt Room Temperature
microhm-mmAt Room Temperature
Hot Rolled
764
1270
Solution Treated
716
1190
Solution Treated and Aged
746
1240
Modulus of Elasticity
Temperature
psi x 10⁶
MPa x 10⁶
°F
°C
80
26.7
31.0
213.7
500
260.0
28.7
197.9
1000
538.0
25.0
172.4
1350
732.0
21.0
144.8
1500
816.0
18.5
127.6
Coefficient of Thermal Expansion
Temperature Range
10⁻⁶/°F
10⁻⁶/°C
80°F to
26.7°C to
200
93
6.7
12.1
600
316
7.5
13.5
1000
538
7.9
14.2
1200
649
8.1
14.6
1600
871
9.0
16.2
Specific Heat Temperature Range
Btu/lb-°F
kJ/kg-K
77/212°F (25/100°C)
0.10-0.11
0.42-0.46
77/1650°F (25/899°C)
0.13
0.54
Heat Treatment
Heat Treatment Method
Process Step
Temperature
Time
Cooling
Method 1 For maximum creep, relaxation and rupture strengthat temperatures above 1100°F (593°C)
Solution Treatment
1800°F (982°C)
Commensurate with thickness
Air cool
Intermediate Age
1550°F (843°C)
24 hrs
Air cool
Final Age
1300°F (704°C)
20 hrs
Air cool
Method 2 For highest room temperature yield strengthand tensile ductility
UNS N07750, W.Nr 2.4669, Inconel X750 (tradename), UNS N07752
Available Forms & Supply Condition
Form
Supply Condition
Bar, Forging, Ring
As-forged / hot-rolled, or solution-treated, with optional grinding/turning
Sheet, Strip, Plate
Hot-rolled or cold-rolled, annealed or solution-treated, pickled/polished
Wire
Solution-treated, or cold-drawn (up to 65% reduction) for smaller diameters
Tube, Coil, Disc
As-rolled or annealed, available in multiple thicknesses and tempers
Workability
The furnace temperature should be 2100°F (1149°C)-for optimal starting temperatures of 1950/2000°F. For service below 1100°F (593°C), higher strength can be obtained by combining some cold work with heat treatment because the effects are additive.
Machinabiliy
Alloy X-750 work hardens quickly and is more difficult to machine than most standard ferritic and martensitic alloys. The alloy is most easily machined in the stress-equalized condition. Because specific cutting forces are high, the machine tools used must have ample power and the cutting speed should be slow. The tools must have smooth finishes, be sharp, and be very rigid. To avoid work hardening , a continuous, smooth cutting action should be maintained; thus, the machines must have a minimum of backlash and the tool and workpiece must be rigidly supported. If at all possible, avoid very small cuts and feeds.
Welding
Alloy X-750 should be welded in the stress-equalized condition, 1625°F (885°C) heat treatment, and solution treated and age hardened after welding has been completed. If this is not practical, the alloy should be welded in the solution-treated condition and age hardened after welding with or without the inclusion of a short-period stress-relieving treatment at 1625°F. Weld joints, because of softening of the alloy within the heat-affected zone, should be located where lower creep properties are required.
Certifications & Quality Assurance
☑ AS 9120B – Aerospace quality management system certification
☑ ISO 9001:2015 – International quality management standard
☑ Full traceability – From melting through final delivery
☑ Complete mill test reports – Available with every shipment
Request a Quote
Contact ZYTC Alloy for professional Inconel X-750 technical datasheets, custom specifications and factory competitive quotations.