Alloy 939 (UNS N09939) Investment-Cast Turbine Blades
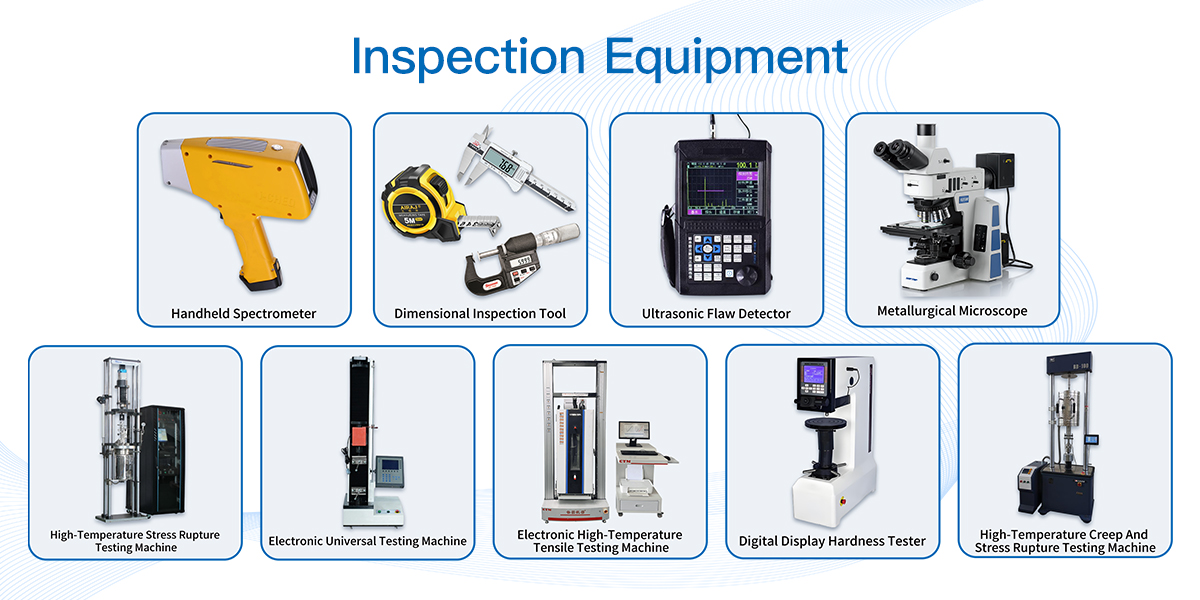
Alloy 939 (UNS N09939 / W.Nr. 2.4635 / GB GH 939), formerly designated INCONEL® alloy 939 (IN 939), is a high-chromium, gamma-prime strengthened nickel superalloy developed in the early 1970s for cast hot-section components. It combines tensile, creep and thermal-fatigue strength at temperatures up to about 850 °C (1560 °F) with oxidation and hot-corrosion resistance that clearly outperforms 16%Cr cast superalloys in sulphur-bearing fuels. Its strengthening system is dual: a high gamma-prime (γ′) volume fraction for precipitation hardening, and one of the highest chromium levels among cast superalloys for environmental resistance. That combination is exactly what industrial and marine gas turbines burning heavy fuel oil or low-calorific gas demand — and it is why Alloy 939 remains a standard material for vanes, blades and combustor hardware decades after its introduction. ZYTC Alloy supplies Alloy 939 as investment castings, machined blanks and AM-ready powder, with vacuum induction melting, full heat treatment, complete traceability and certified test reports for every lot. Quick Facts
Chemical Composition (typical, weight %)
Si and Mn are controlled to low residuals (commonly ≤0.3 and ≤0.2 %); all trace elements are limited per the applicable purchase specification. Unlike many second-generation cast superalloys, Alloy 939 contains essentially no molybdenum — tungsten is the solid-solution strengthener. Nominal values above follow the published alloy definition; acceptance limits are those of the order specification or OEM process spec, not these nominal figures. Physical Properties (typical)
Values are typical literature and supplier data for the fully heat-treated condition; they vary with casting route and microstructure and are provided as a design guide only. Mechanical Properties (cast + fully heat-treated, typical)
Acceptance values are those stated in the purchase order and the applicable OEM process specification; request the certified test report for the actual lot. Hot-section castings are normally qualified by individual OEM specs rather than by a general-purpose bar/plate standard. Heat TreatmentAlloy 939 reaches its design strength only after a full precipitation-hardening sequence; the as-cast (or as-built AM) structure is not the delivery condition. Representative cycles:
Exact schedules must follow the applicable process specification and component geometry. Solution treatment also dissolves undesirable phases that form during solidification. As-built LPBF material contains insufficient γ′; without the full sequence it will not reach design strength. Alloy 939 vs Alloy 738LC — which one for your turbine?
Rule of thumb: clean fuel → Alloy 738LC; corrosive, sulphur-rich fuel or marine environment → Alloy 939. The higher chromium also reduces the reliance on protective coatings, which lowers lifetime maintenance cost on industrial frames. Applications
Welding & RepairAlloy 939 is repair-weldable with precautions: the high γ′ content makes it prone to microfissuring in the heat-affected zone. Successful repair of vane and blade castings requires preheat, low-energy welding parameters and a full post-weld heat treatment. New fabrication welds are limited; design castings so that critical joints are avoided or machined afterwards. Specifications — read this before comparing quotationsAlloy 939 is not covered by a general-purpose AMS or ASTM bar/plate specification. Beware of datasheets quoting “AMS 5400” — that SAE number covers a 15Cr stainless investment casting, not this alloy. In practice Alloy 939 is procured against OEM process specifications (turbine-maker vane and blade specs), national designations (UNS N09939, W.Nr. 2.4635, GB GH 939) or, for additive manufacturing, against AM material specifications. We test to the specification called out on your drawing; if your drawing references an OEM spec number, send it with the RFQ. |