ASTM B333 / UNS N10665 (Alloy B-2) Nickel-Molybdenum Alloy Plate
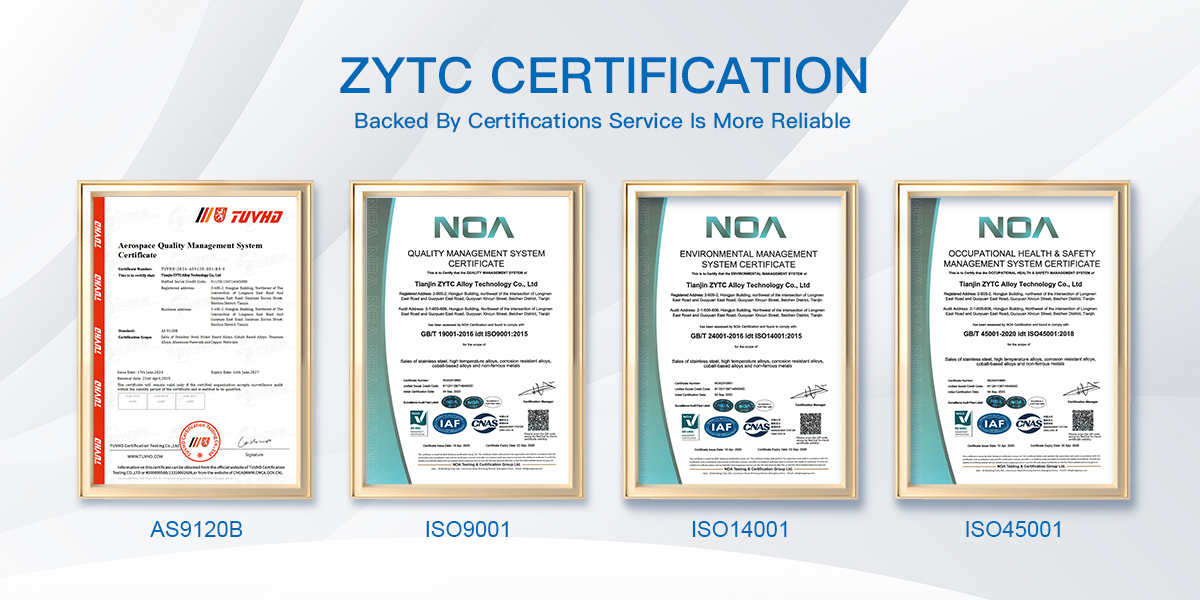
ASTM B333 UNS N10665 (Alloy B-2) Nickel-Molybdenum Plate — Welding Process, Deformation, and Contamination ControlFor hydrochloric, sulfuric, and phosphoric acid equipment design engineers and buyers — supplied by ZYTC Alloy, a China-based nickel alloy manufacturer and exporter, ISO 9001 certified B-2 Failures Are Rarely About the Material ItselfAlloy B-2 (UNS N10665) is a nickel-molybdenum alloy designed specifically for extreme reducing environments, with excellent resistance to hydrochloric, sulfuric, and phosphoric acids and other non-oxidizing acids. Its high molybdenum content (26–30%) allows it to maintain good resistance to intergranular attack even in the as-weldedcondition. But a fact that recurs in chemical equipment procurement is this: most B-2 failures are not the result of choosing the wrong material — they are the result of process decisions made during fabrication. The wrong welding method, cold forming without proper heat treatment, or iron or copper contamination in the system — any one of these three is enough to make B-2 fail prematurely in an environment it should have handled. The three variables below are what need to go into the technical agreement when purchasing B-2 plate. ZYTC Alloy supplies B-2 plate, sheet, and strip from China with full traceability and process-matched supply conditions. Variable 1: Welding Method Selection —"Weldable"Is Not EnoughAlloy B-2 can be welded by GTAW (TIG), GMAW (MIG), and SMAW (stick electrode), with matching filler metal ERNiMo-7 (or equivalent B-2 filler). Post-weld heat treatment is usually not required, provided weld heat input is kept within a reasonable range. But there is a key limitation: the heat input of submerged arc welding (SAW) may be too high for B-2. Excessive heat input reduces corrosion resistance in the heat-affected zone (HAZ), and certain production heats are more sensitive to this than others. Procurement action: Specify the welding method in the technical agreement. If the fabricator plans to use SAW, require HAZ corrosion resistance verification data or a switch to GTAW/GMAW. Do not accept a general statement that"B-2 is weldable"— the welding method directly affects equipment life in hydrochloric acid service. Variable 2: Cold Forming Beyond 7% Deformation Requires Solution AnnealingAfter cold forming (rolling, stamping, bending), if the outer fiber elongation exceeds 7%, B-2 plate must be solution annealed (1066–1177°C, water quench) before subsequent welding or service. This threshold is not a recommendation — it is a process requirement. Residual stress and dislocation structure introduced by cold forming, if not removed by solution treatment, can readily cause cracking during the thermal cycle of subsequent welding — and the cracks may only appear after the equipment is in service, causing unplanned shutdown and rework. Procurement action: If equipment fabrication involves cold rolling or cold forming, require the fabricator to record the cold forming deformation in the PO or technical agreement. For components approaching or exceeding 7%, require solution treatment records (temperature, holding time, cooling method). Do not assume"the supplier will handle it"— many fabricators skip this step to save cost or schedule. Variable 3: Iron and Copper Contamination — The Hidden Cause of B-2 Failure in Reducing AcidsB-2 is not resistant to oxidizing acids, and this is usually noted during material selection. But a more insidious risk is this: even in reducing acids such as hydrochloric acid, if iron or copper ions contaminate the system, B-2 will fail prematurely. Contamination sources include corrosion products from carbon steel piping or supports, corrosion of copper alloy valves or gaskets, and weld spatter or grinding tool residue. These contaminants create localized oxidizing conditions in the acid, disrupting B-2's passive state. Procurement action: Specify in the equipment design and fabrication specification that piping, valves, gaskets, and tooling in contact with B-2 must not use copper alloys or carbon steel. Welding and grinding tools should be dedicated or thoroughly cleaned. For critical equipment, an iron contamination test (e.g., ferrocyanide test) before commissioning is recommended. Chemical Composition (UNS N10665)
Low carbon (≤0.02%) and low silicon (≤0.10%) are the basis for B-2's as-welded intergranular corrosion resistance. Iron and chromium limits (Fe ≤2.0, Cr ≤1.0) are controlled to avoid formation of harmful secondary phases in reducing acids. Mechanical Properties (Annealed Plate)
An Overlooked Processing Limit: The Intermediate-Temperature Sensitization RangeProlonged exposure of B-2 to the 538–871°C (1000–1600°F) range forms secondary phases that reduce toughness. This temperature range overlaps with parts of the cooling cycle in some heat treatments and welding operations. Procurement action: If fabrication involves holding in this temperature range (e.g., stress relief or preheat), specify the holding time and cooling method in the technical agreement. For components requiring heat treatment after cold forming, prefer solution annealing (1066–1177°C) over intermediate-temperature stress relief. Supply Specifications from ZYTC Alloy
Condition confirmation: The certificate states the solution-annealed condition and cooling method. If the plate will be used for components that are cold-formed and then welded directly, note this in the inquiry — as a China-based manufacturer, ZYTC can confirm whether the incoming residual stress condition suits the downstream process before shipping. Typical Applications (Require Correct Fabrication Practice)Hydrochloric and sulfuric acid pressure vessels and reactors. The core application for B-2. Preconditions: correct welding method, solution annealing based on cold forming deformation, and no iron or copper contamination in the system. Heat exchangers, piping, pumps, and valves. Components in contact with the corrosive medium. Note that seals and gaskets in pumps and valves must not be copper alloys. FGD system components. Reducing zones in flue gas desulfurization. Confirm whether oxidizing species (such as chlorine or nitrates) are present in the medium; if so, B-2 is not suitable. Why Source B-2 from ZYTC Alloy
Request a QuotePlease provide: thickness, width, length, quantity, downstream process (cold forming / welding / direct service), welding method (if known), and whether measured chemistry or third-party testing is required. If the equipment involves cold rolling or submerged arc welding, note this in the inquiry — ZYTC will confirm incoming condition and process compatibility rather than shipping"B-2 plate"by grade name alone. 📧 daisy@zytcsteel.com |