UNS N07740 / Alloy 740H / 2.4663 - ZYTC Alloy
UNS N07740 / Alloy 740H / 2.4663 — Precipitation-Hardenable Nickel Superalloy for A-USC Power
ZYTC Alloy is an ISO 9001 & AS 9120B certified manufacturerofInconel® 740H (UNS N07740), a gamma-prime strengthened Ni-Cr-Co superalloy engineered for advanced ultra-supercritical (A-USC) boilers. Available as bar, forgings and seamless tube with full batch traceability and in-house lab verification. Request a free quote and technical data today.
Model No: Alloy 740H | Delivery: FOB | Minimum Order: 50 kilograms | Supply Ability: 5000 kilograms / Month | Stock Time: 7-10 Days | Country of Origin: CHINA
PRODUCT DESCRIPTION
ZYTC Alloy 740H (UNS N07740) — Precipitation-Hardenable Nickel-Cobalt-Chromium Superalloy. As an ISO 9001 and AS 9120B certified supplier, ZYTC Alloy presents this technical guide for Inconel® 740H for confident material evaluation.
I. Product Information
- Material Name: Inconel® 740H Nickel-Chromium-Cobalt Superalloy (UNS N07740 / W.Nr. 2.4663)
- Material Definition: A precipitation-hardenable Ni-Cr-Co superalloy strengthened by gamma-prime (γ′) phase, developed specifically for advanced ultra-supercritical (A-USC) steam service at 700–800 °C.
- Core Value Proposition: The only nickel alloy code-qualified for A-USC boiler construction under ASME Code Case 2702, with a maximum use temperature of 800 °C (1472 °F) and 100,000-hour creep-rupture strength at 750 °C / 35 MPa.
- Key Advantages: Gamma-prime (γ′) strengthening | Excellent creep-rupture strength to 800 °C | Superior coal-ash and steam oxidation resistance | Good weldability with controlled PWHT | ASME Code Case 2702 approved
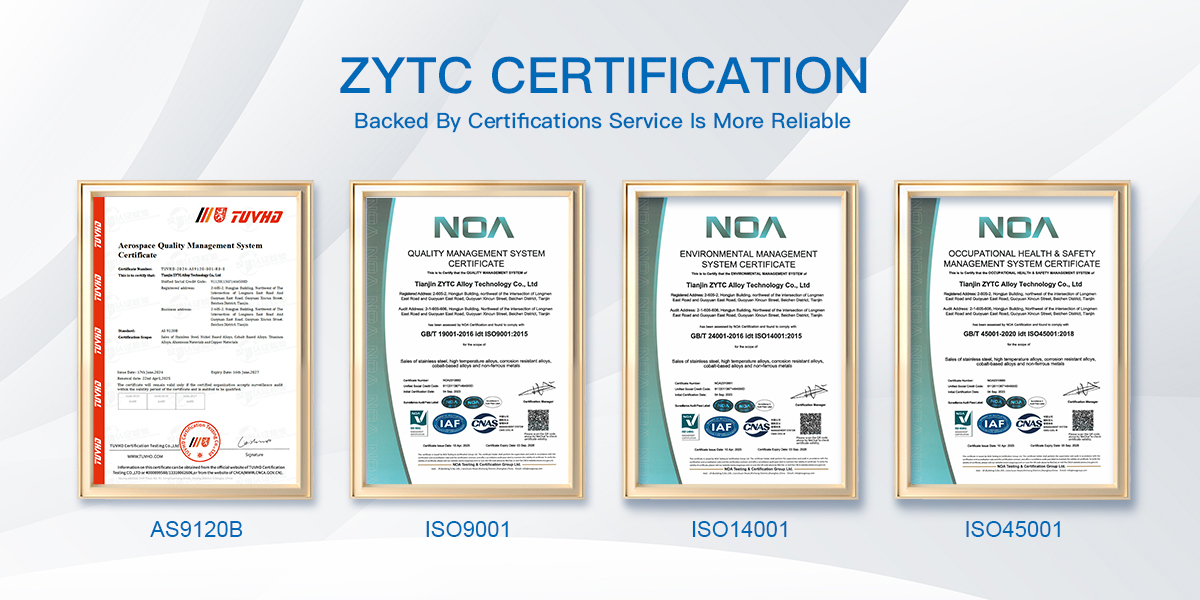
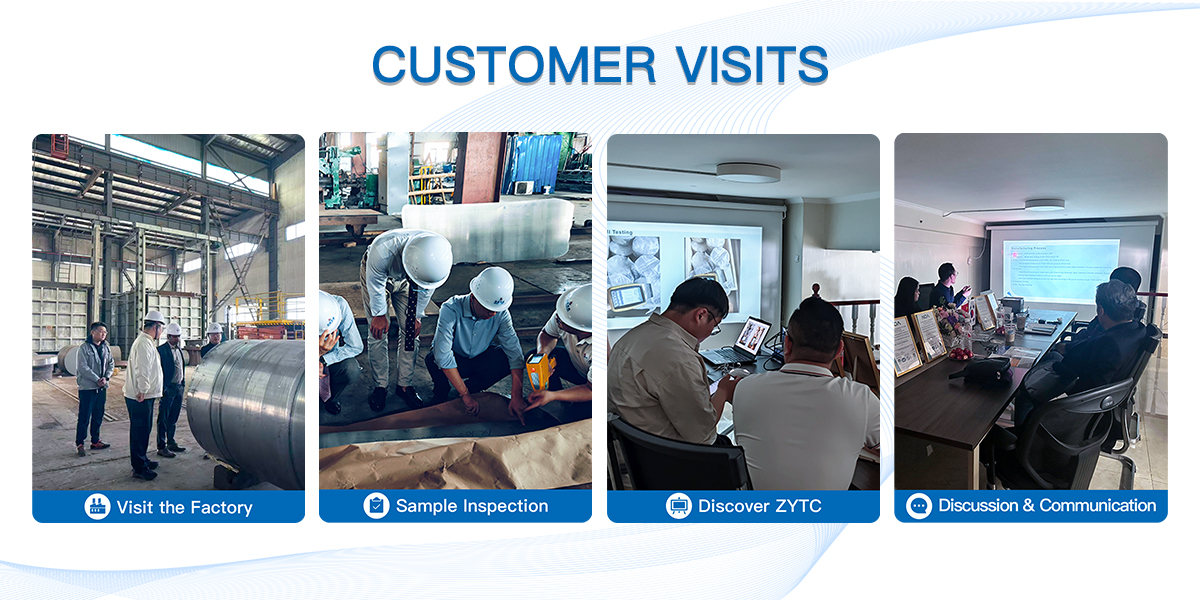
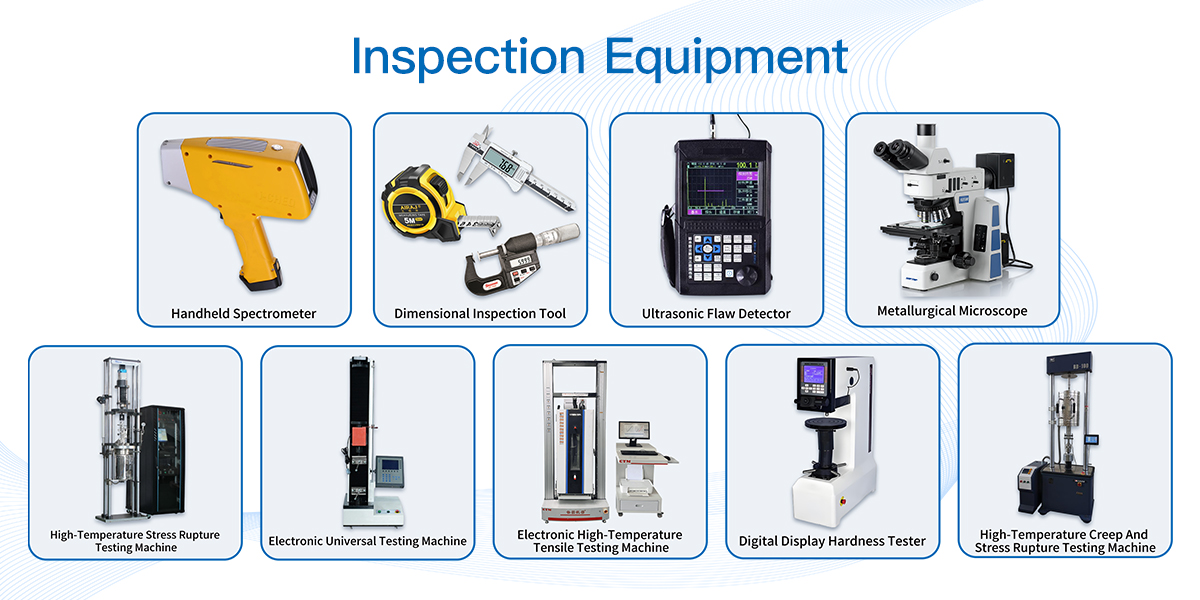
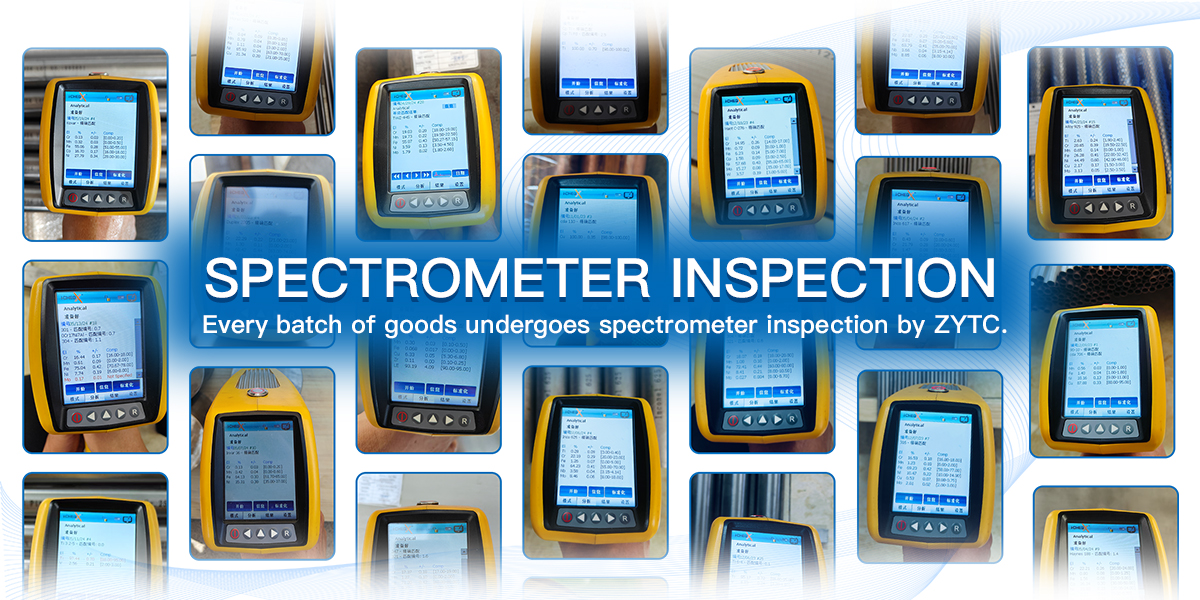
- Certification:ISO 9001 and AS 9120B certified; full batch traceability; in-house laboratory verification.
- Product Forms: Bar & Rod | Forgings & Rings | Seamless Pipe & Tube | Plate | Welding Wire
If you need a size, temper, heat-treatment condition or certification that is not listed below, send us the drawing — we will confirm mill capability and lead time within one working day.
II. Material Standards & Specifications
| Standard / Specification | Product Form | Description |
|---|---|---|
| UNS N07740 | – | Unified numbering system |
| ASTM B983 / ASME SB983 | Bar, forgings, seamless tube | Precipitation-hardened Ni-Cr-Co alloy – current edition |
| ASME Code Case 2702 | Sheet, plate, rod, seamless pipe & tube, fittings, forgings | A-USC boiler construction, Section I & B31.1 – max 800 °C |
| AWS A5.14 ERNiCrCoMo-1 | Welding filler | Matching filler metal for 740H |
| EN 10204 3.1 | Mill certificate | 3.2 / third-party inspection available on request |
Material must be supplied in the solution heat-treated and aged condition. ASME Code Case status and revisions should be confirmed with ASME before specification.
III. Chemical Composition (wt%)
| Element | Min | Max |
|---|---|---|
| Nickel (Ni) | Balance | – |
| Chromium (Cr) | 23.5 | 25.5 |
| Cobalt (Co) | 15.0 | 22.0 |
| Niobium (Nb) | 0.50 | 2.50 |
| Titanium (Ti) | 1.15 | 1.65 |
| Aluminum (Al) | 1.20 | 1.75 |
| Molybdenum (Mo) | 0.30 | 2.00 |
| Carbon (C) | 0.02 | 0.08 |
| Manganese (Mn) | – | 0.50 |
| Silicon (Si) | – | 1.00 |
| Phosphorus (P) | – | 0.030 |
| Sulfur (S) | – | 0.015 |
IV. Service Conditions & Material Selection Boundaries
Suitable Conditions
- Advanced ultra-supercritical (A-USC) superheater and reheater tubing at 700–800 °C
- Thick-section steam headers and main steam piping above 700 °C
- Pressure-containing components exposed to coal-ash corrosion and high-temperature steam oxidation
- Concentrated solar power receivers and high-temperature salt-loop tubing
Typical Applications
- Power Generation: A-USC boiler tubes, steam headers, main steam piping, turbine components
- Oil & Gas / Petrochemical: High-temperature pressure piping and heat exchangers
- Concentrated Solar: Receiver and molten-salt loop components
Selection Boundaries
- Below 700 °C / cost-sensitive service: consider Inconel® 617 or Alloy 800H
- Severe aqueous corrosion: consider Inconel® 625 or Hastelloy® C-276
- Maximum strength at moderate temperature: consider Alloy 718
V. Manufacturing Process & Heat Treatment
| Process | Parameters | Outcome |
|---|---|---|
| Solution Anneal | ≥ 1100 °C (2010 °F), 1 hr per 25 mm thickness (min 0.5 hr), rapid cool | Dissolves γ′, recrystallizes |
| Aging | 760–815 °C (1400–1500 °F), min 4 hr up to 50 mm thickness | γ′ precipitation, peak strength |
| Post-Weld Heat Treatment | 760–815 °C (1400–1500 °F), mandatory per Code Case 2702 | Restores properties in weld zone |
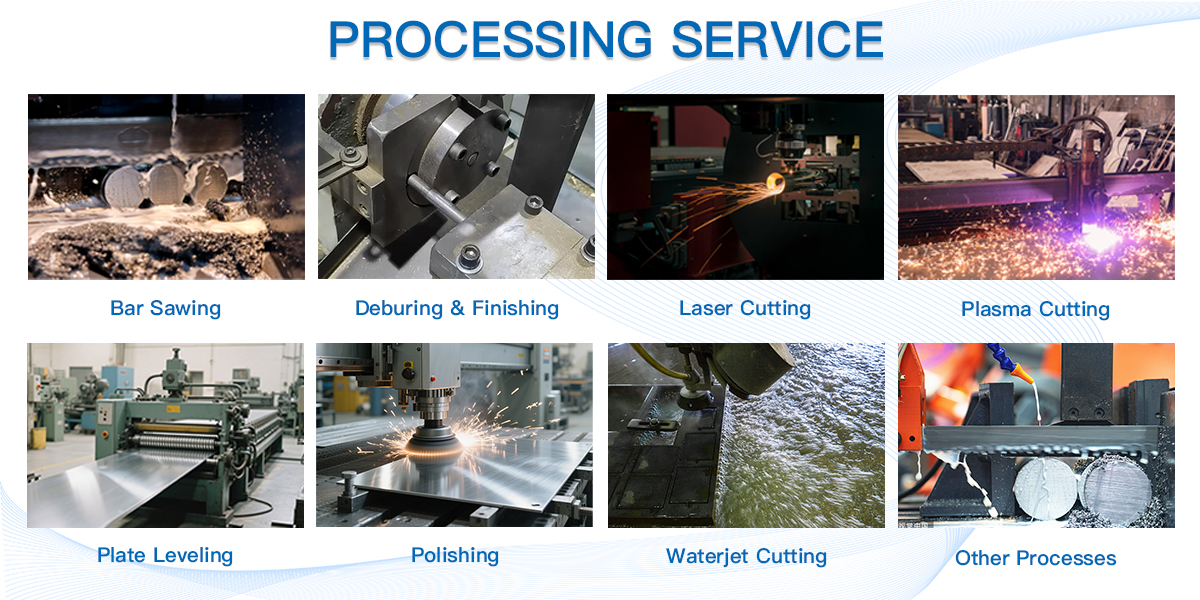
Fabrication: Welding by GTAW / SAW with matching ERNiCrCoMo-1 filler; PWHT is mandatory; a weld strength reduction factor of 0.70 applies above 600 °C for longitudinal seams. Hot working at 1050–1150 °C. Cold forming above 5 % strain requires full solution + aging re-treatment of the entire component. Machining with rigid setups, positive feeds and sharp carbide tooling.
VI. Mechanical Properties
Condition: Solution Treated + Aged (Room Temperature)
| Property | Typical / Minimum Value |
|---|---|
| Tensile Strength | ≥ 1000 MPa (145 ksi) |
| Yield Strength (0.2 % offset) | ≥ 620 MPa (90 ksi) |
| Elongation | ≥ 20 % |
| Hardness | Contact for certified test reports |
Elevated-Temperature Tensile (transverse, aged):
| Temperature | Yield Strength | Tensile Strength |
|---|---|---|
| 700 °C (1292 °F) | 567 MPa (82.2 ksi) | 861 MPa (124.9 ksi) |
| 750 °C (1382 °F) | 596 MPa (86.4 ksi) | 818 MPa (118.6 ksi) |
| 800 °C (1472 °F) | 594 MPa (86.2 ksi) | 691 MPa (100.2 ksi) |
Design stress values (Su, Sy) per ASME Code Case 2702 Tables 5/5M and 6/6M. Certified test reports available on request.
VII. Material Comparison Guide
| Dimension | Alloy 740H | Alloy 617 | Alloy 625 | Alloy 718 |
|---|---|---|---|---|
| Primary Strength | Creep strength to 800 °C | Solid-solution strength | Corrosion + strength | Highest strength to 704 °C |
| Strengthening | Gamma-prime (γ′) | Solid-solution | Solid-solution | Gamma-double-prime (γ″) |
| Max Use Temperature | 800 °C (code-approved) | ~980 °C | ~980 °C | ~704 °C |
| Coal-Ash Corrosion | Excellent | Good | Moderate | Poor |
| Weldability | Good (with PWHT) | Excellent | Excellent | Excellent |
| Typical Use | A-USC boilers, steam piping | Gas turbines, chemical | Marine, chemical, FGD | Aerospace, oil & gas tools |
Procurement Recommendation:ChooseInconel® 740H for A-USC boiler and steam piping where code-approved creep strength and coal-ash corrosion resistance above 700 °C are required. Choose Alloy 617 for lower-cost high-temperature service without code qualification. Choose Alloy 625 for severe aqueous corrosion. Choose Alloy 718 for maximum room/moderate-temperature strength and easier fabrication.
Request a Quote or Sample Today
For A-USC power generation and high-temperature pressure applications demanding Inconel® 740H performance, contact ZYTC Alloy today. Our technical team is ready to assist with material selection, heat treatment specification and code compliance.
Contact Us: Email: daisy@zytcsteel.com | WhatsApp / WeChat: +86 17335753350
Procurement Recommendation: ChooseInconel®740H for A-USC boiler and steam piping where code-approved creep strength and coal-ash corrosion resistance above 700 °C are required. Choose Alloy 617 for lower-cost high-temperature service without code qualification. Choose Alloy 625 for severe aqueous corrosion. Choose Alloy 718 for maximum room/moderate-temperature strength and easier fabrication. Request a Quote or Sample Today For A-USC power generation and high-temperature pressure applications demanding Inconel®740H performance, contact ZYTC Alloy today. Our technical team is ready to assist with material selection, heat treatment specification and code compliance. Contact Us: Email: daisy@zytcsteel.com | WhatsApp / WeChat: +86 17335753350 |