UNS N07792 / Alloy 792 / GH792
UNS N07792 / Alloy 792 / GH792 High-Strength Cast Nickel-Base Superalloy for Turbine Hot Sections CAST SUPERALLOY GAMMA-PRIME STRENGTHENED AEROSPACE GRADE |
N07792 UNS Designation | 8.10 g/cm³ Density | ~1050 °C Max Service Temp | ~65% Gamma-Prime Volume | Investment Cast Process |
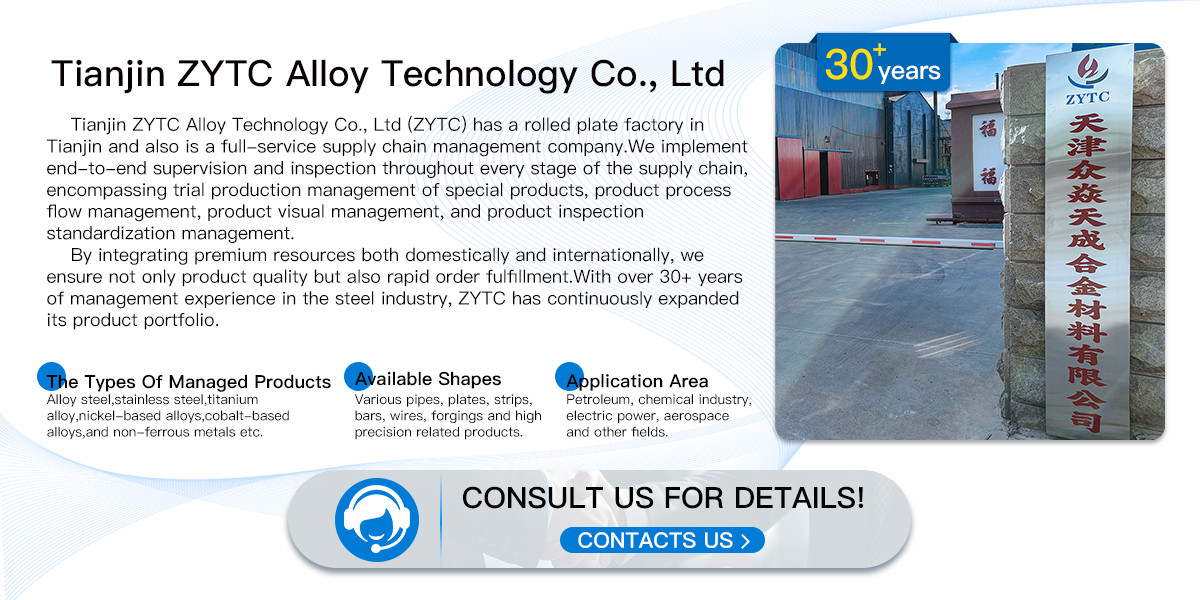
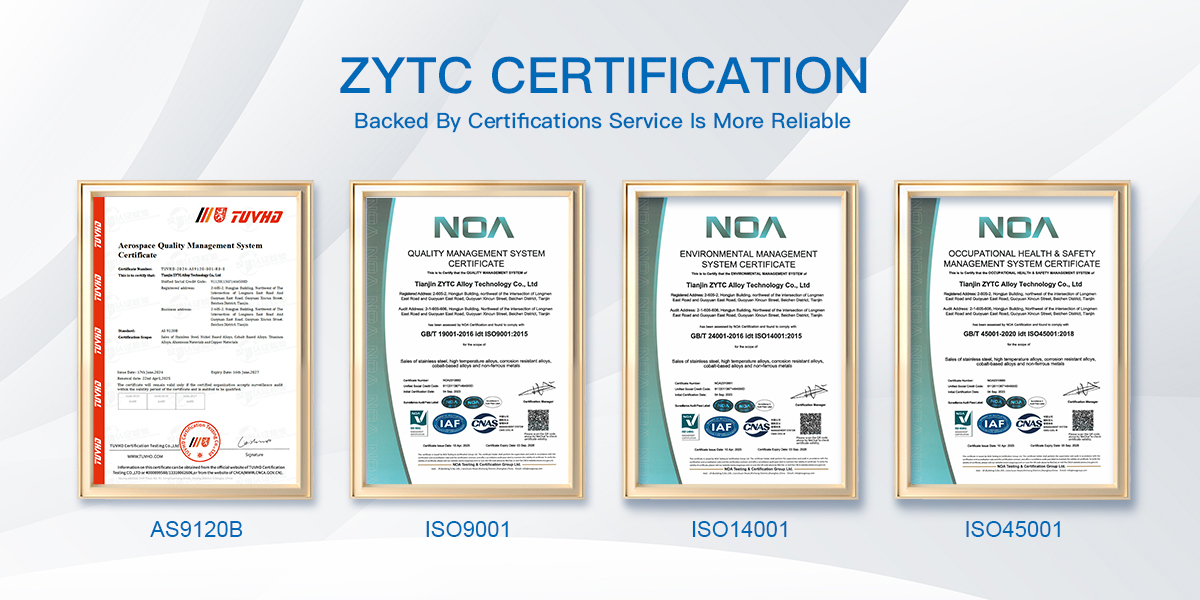
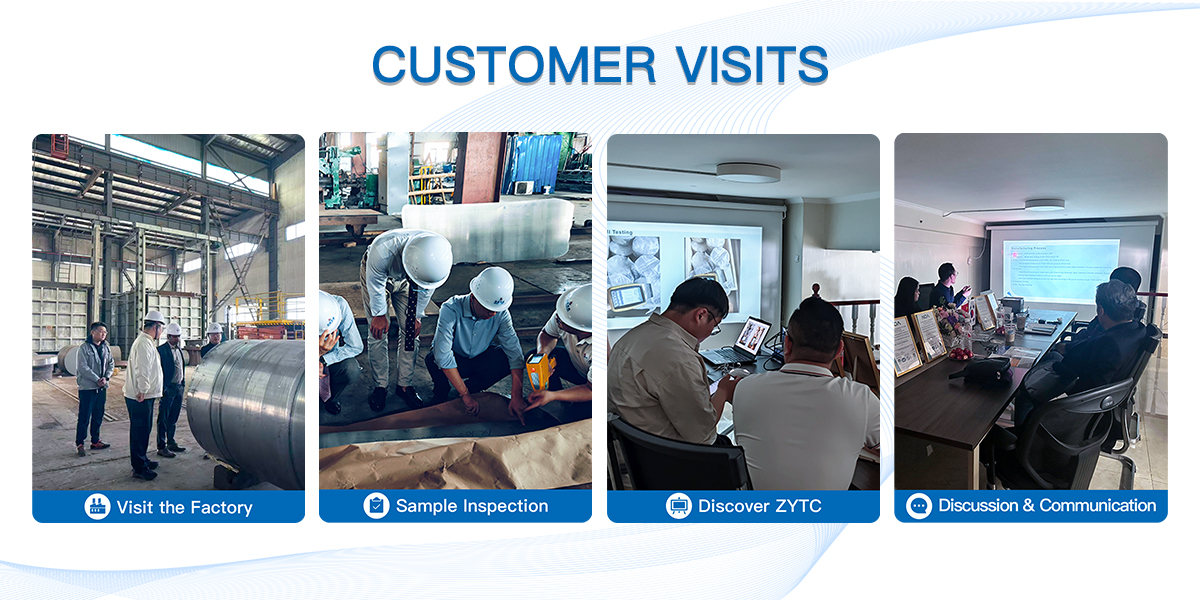
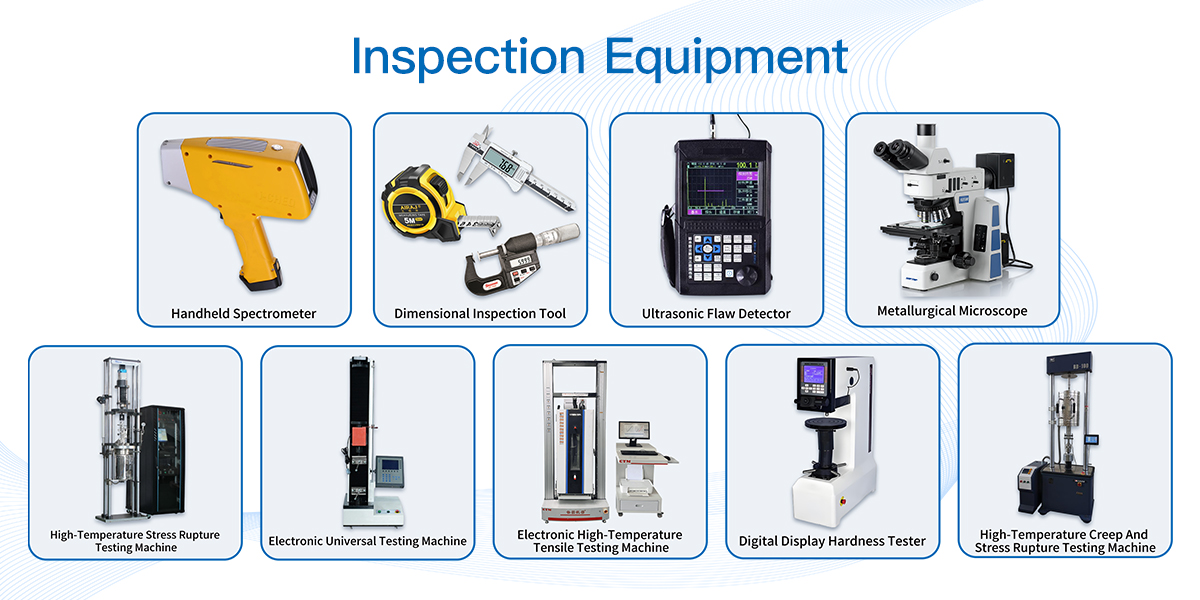
ZYTC Alloy is an ISO 9001 and AS 9120B certified manufacturer and supplier of Inconel® 792 (UNS N07792), a precipitation-hardened cast nickel-base superalloy designed for long-term service at 900–1050 °C in aerospace and gas-turbine hot sections. Strengthened by an exceptionally high gamma-prime (γ′) volume fraction of about 65%, it delivers outstanding creep-rupture strength, thermal-fatigue resistance and oxidation/hot-corrosion resistance. We supply investment castings, master alloy and made-to-drawing components with full batch traceability and in-house laboratory verification.
Note: Inconel® 792 is a casting alloy. It is supplied as investment castings, master alloy ingots, cast bars and finished machined parts — it is not produced as seamless tube. Confirm product form and applicable specification before ordering.
I. Product Overview
Inconel® 792 is a vacuum-induction-melted, precipitation-hardened cast superalloy. Its high volume fraction of γ′ (Ni₃Al/Ti-type) precipitate is the principal source of high-temperature strength, while chromium and aluminum provide oxidation and sulfidation protection and cobalt, tungsten, molybdenum and tantalum contribute to solid-solution strengthening, creep resistance and microstructural stability. It is optimized for precision investment casting of complex, thin-wall components followed by CNC machining.
II. Key Advantages
Ultra-High γ′ Content About 65% gamma-prime fraction provides long-term strength retention and creep resistance at 900–1000 °C. | Thermal Fatigue Resistance Cobalt addition stabilizes γ′ and improves resistance to thermal cycling in start-stop turbine service. | Oxidation & Hot Corrosion Chromium and aluminum form protective Cr₂O₃ / Al₂O₃ scales in combustion and exhaust environments. |
Excellent Castability Designed for investment casting of thin-wall, intricate geometries with low porosity and uniform microstructure. | Structural Stability Tungsten, molybdenum and tantalum provide solid-solution strengthening and resist γ′ coarsening. | Precision Machinable Cast + aged parts can be CNC finished to tight tolerances and fine surface finishes. |
III. Chemical Composition
| Element | Typical / Specified Range (wt%) | Primary Function |
|---|---|---|
| Nickel (Ni) | Balance (~58–63) | Matrix; high-temperature strength |
| Chromium (Cr) | 12.0 – 14.0 | Oxidation & hot-corrosion resistance |
| Cobalt (Co) | 9.0 – 11.0 | γ′ stabilization; thermal-fatigue resistance |
| Aluminum (Al) | 3.4 – 4.0 | Primary γ′ former; age hardening |
| Titanium (Ti) | 3.8 – 4.3 | γ′ strengthening |
| Molybdenum (Mo) | 1.5 – 2.5 | Solid-solution strengthening |
| Tungsten (W) | 3.5 – 4.5 | Creep resistance |
| Tantalum (Ta) | 3.5 – 4.2 | γ′ strengthening; creep resistance |
| Carbon (C) | 0.10 – 0.15 | Grain-boundary carbide formation |
| Boron (B) | 0.005 – 0.015 | Grain-boundary strengthening |
| Zirconium (Zr) | ≤ 0.05 | Grain-boundary stability |
| Silicon (Si) | ≤ 0.50 | Casting & oxidation behavior |
| Manganese (Mn) | ≤ 0.50 | Melting / casting control |
Composition values are typical references compiled from public sources. Guaranteed limits are those stated on the applicable specification and the EN 10204 3.1 mill test certificate supplied with each lot.
IV. Physical & Mechanical Properties
Physical Properties
| Physical Property | Typical Value | Condition / Method |
|---|---|---|
| Density | 8.10 g/cm³ | ASTM B311 |
| Melting Range | 1260 – 1335 °C | Supplier data |
| Thermal Conductivity | 10.9 W/m·K | at 100 °C; ASTM E1225 |
| Electrical Resistivity | 1.32 µΩ·m | at 20 °C; ASTM B193 |
| Thermal Expansion | 13.5 µm/m·°C | 20–1000 °C; ASTM E228 |
| Specific Heat | 445 J/kg·K | at 20 °C |
| Elastic Modulus | ~185 GPa | at 20 °C |
Mechanical Properties (Cast + Aged)
| Mechanical Property | Typical Value (Cast + Aged) | Method |
|---|---|---|
| Ultimate Tensile Strength | 880 – 1020 MPa | ASTM E8/E8M |
| Yield Strength (0.2% offset) | 700 – 800 MPa | ASTM E8/E8M |
| Elongation | 3 – 6% (25 mm gauge) | ASTM E8/E8M |
| Hardness | 330 – 400 HB | ASTM E10 |
| Creep Rupture Strength | ≥ 140 MPa @ 870 °C / 1000 h | ASTM E139 |
| Max Continuous Service | ~1050 °C | Application reference |
Mechanical data are typical values for investment-cast, solution-treated and aged condition. Values vary with casting process, section thickness and heat treatment. Certified test reports are available on request.
V. Standards & Specifications
| Standard / Specification | Scope |
|---|---|
| UNS N07792 | Unified Numbering System designation |
| GH792 / GB/T 14992 | Chinese designation for cast nickel-base superalloy |
| Customer / OEM Specifications | Aerospace castings are commonly supplied to specific engine-maker (e.g. PWA) or customer drawings |
| EN 10204 3.1 | Mill test certificate (3.2 / third-party inspection on request) |
VI. Typical Applications
Aerospace Engines Turbine blades and vanes, nozzle guide vanes (NGV), blade platforms, tip shrouds, combustor hardware, afterburner components. | Power Generation Industrial and utility gas-turbine blades and stator vanes, transition ducts, high-temperature seals and casings. |
Marine & Oil & Gas Marine propulsion turbine hot-section parts, oil- and gas-fired turbine components. | Industrial Heat Furnace hardware, heat shields, and components in corrosive / carburizing atmospheres. |
VII. Manufacturing & Heat Treatment
| Process | Representative Parameters | Purpose |
|---|---|---|
| Solution Treatment | ~1120 °C / 2 h / air cool | Dissolve γ′ and homogenize the cast structure |
| Aging | ~840 °C / 24 h / air cool | Precipitate γ′ for peak strength |
| Hot Isostatic Pressing (HIP) | Per casting requirement | Close internal porosity, improve fatigue life |
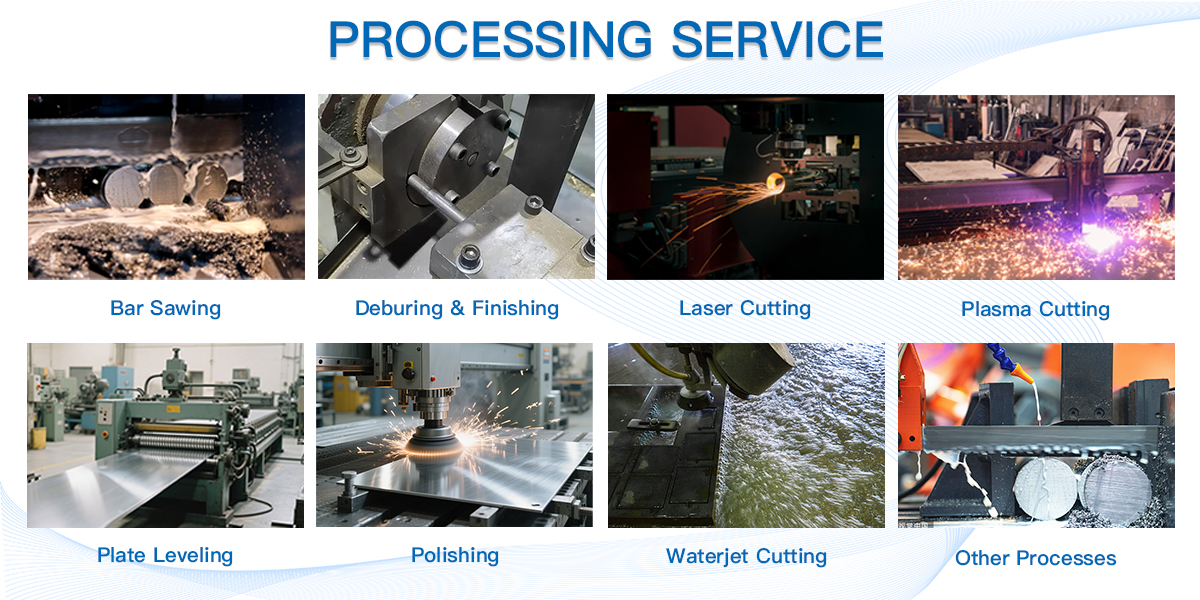
| CNC Machining | After heat treatment | Achieve final dimensional and surface tolerances |
Heat-treatment parameters above are representative literature values. Actual cycles must be confirmed against the applicable material specification and production qualification requirements. Post-cast HIP is recommended for critical rotating parts.
VIII. Material Comparison & Selection Guide
Alloy 792 (IN-792) Cast, γ′ ≈ 65%. Highest strength + hot corrosion balance for turbine blades and vanes; service to ~1050 °C. | Alloy 713C Cast, lower cost. Good castability for turbocharger and turbine wheels; moderate hot-corrosion resistance. |
IN-738 / IN-738LC Cast, strong hot-corrosion resistance; widely used in industrial gas-turbine hot sections. | Alloy 718 Wrought / cast, γ″ strengthened. Excellent fabricability and weldability; limited to ~704 °C. |
Procurement guidance:ChooseInconel® 792 when a cast blade/vane needs the highest combination of creep strength and hot-corrosion resistance near 1000 °C. Choose Alloy 713C for cost-sensitive cast parts with moderate duty. Choose IN-738 where hot corrosion dominates (e.g. industrial / marine gas turbines). Choose Alloy 718 when wrought form, weldability and lower-temperature strength are required.
IX. Supply Forms & Quality Assurance
| Item | Detail |
|---|---|
| Available Forms | Investment castings (blades, vanes), master alloy ingots, cast bars / rods, rings, finished machined parts to drawing |
| Delivery Condition | Investment cast, solution-treated and aged (or per customer specification) |
| Quality Documents | EN 10204 3.1 mill test certificate; chemical & mechanical test reports; NDT / radiography on request |
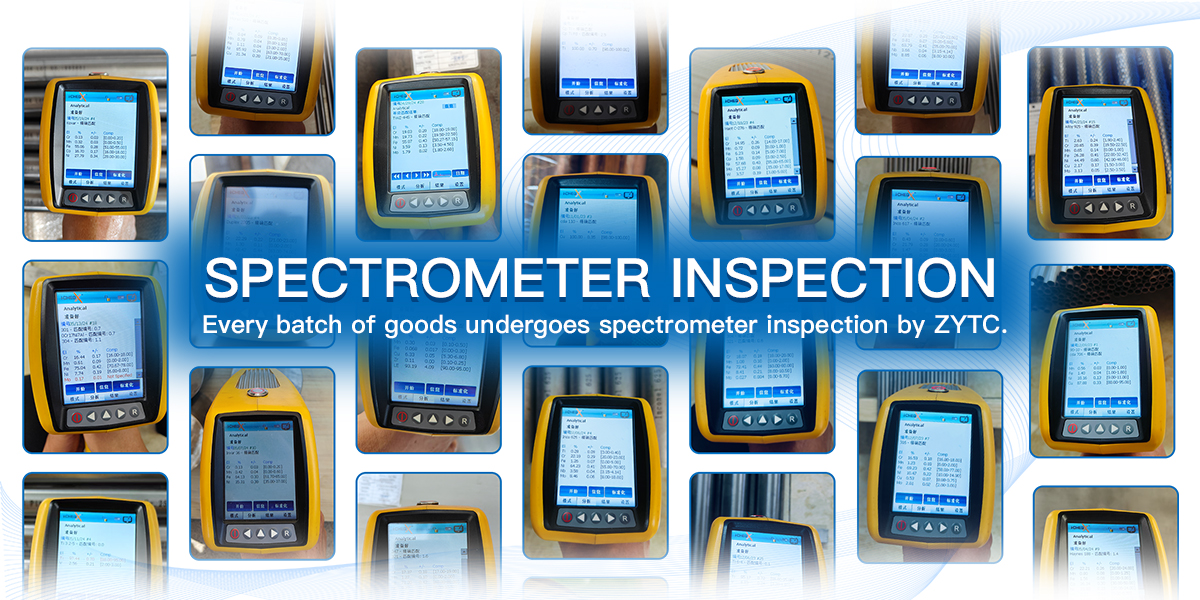
| Traceability | Full heat-lot traceability with in-house laboratory verification |
| Lead Time | Standard items 7–20 days; made-to-drawing / bulk 25–45 days |
| Certification | ISO 9001 and AS 9120B certified manufacturer |
Request a Quote or Sample Today For turbine hot-section components demanding Inconel® 792 performance, contact ZYTC Alloy. Our technical team is ready to assist with material selection, casting and heat-treatment specification, and specification compliance. Email: daisy@zytcsteel.com | WhatsApp / WeChat: +86 17335753350 |