Alloy PE11 (UNS N09901 / 2.4662) is a precipitation-hardenable nickel-iron-chromium superalloy that combines both precipitation hardening and solid-solution strengthening mechanisms through strategic additions of aluminum, titanium, and molybdenum . Developed specifically for service around 550°C (1020°F), it delivers high tensile strength, excellent ductility, and good oxidation resistance, making it a reliable and cost-effective solution for gas turbine and industrial furnace applications .
1. Product Specifications & Physical DataZYTC Alloy supplies UNS N09901 in comprehensive mill forms for aerospace, power generation, and industrial processing applications requiring verified mechanical properties and complete material traceability. Available Forms: Sheet, plate, round bar, flat bar, forging stock, wire, and welding wire . Specifications: DTD 5037, AFNOR Z8 NC D38, MSRR 7182, MSRR 7181, WS 2.4662 .
| Chemical Composition (Weight %) | Nimonic® PE11 Specification |
|---|
| Nickel (Ni) | 37.0 - 41.0 | | Iron (Fe) | 32 (Balance) | | Chromium (Cr) | 17.0 - 19.0 | | Molybdenum (Mo) | 4.75 - 5.75 | | Titanium (Ti) | 2.20 - 2.50 | | Aluminum (Al) | 0.70 - 1.00 | | Cobalt (Co) | 1.0 max. | | Zirconium (Zr) | 0.020 - 0.050 | | Carbon (C) | 0.030 - 0.080 | | Boron (B) | 0.0010 max. | | Manganese (Mn) | 0.20 max. | | Silicon (Si) | 0.50 max. | | Copper (Cu) | 0.50 max. | | Sulfur (S) | 0.015 max. |
| Physical Properties | Metric | Imperial |
|---|
| Density | 8.02 g/cm³ | 0.290 lb/in³ | | Melting Range | 1280 - 1350°C | 2340 - 2460°F |
| Mechanical Properties (Precipitation Hardened) | Metric | Imperial |
|---|
| Tensile Strength (RT) | 1060 MPa | 154,000 psi | | Yield Strength (0.2% offset, RT) | 700 MPa | 102,000 psi | | Elongation at Break (RT) | 20% | 20% |
2. Fabrication & Material ComparisonNimonic® PE11 offers good fabricability with appropriate techniques, though its strength requires more powerful equipment than standard steels . Heat Treatment : Solution Anneal: 1021°C (1870°F) × 2 hours, air cool Secondary Treatment: 799°C (1470°F) × 2 hours, air cool Final Age: 699°C (1290°F) × 16 hours, air cool
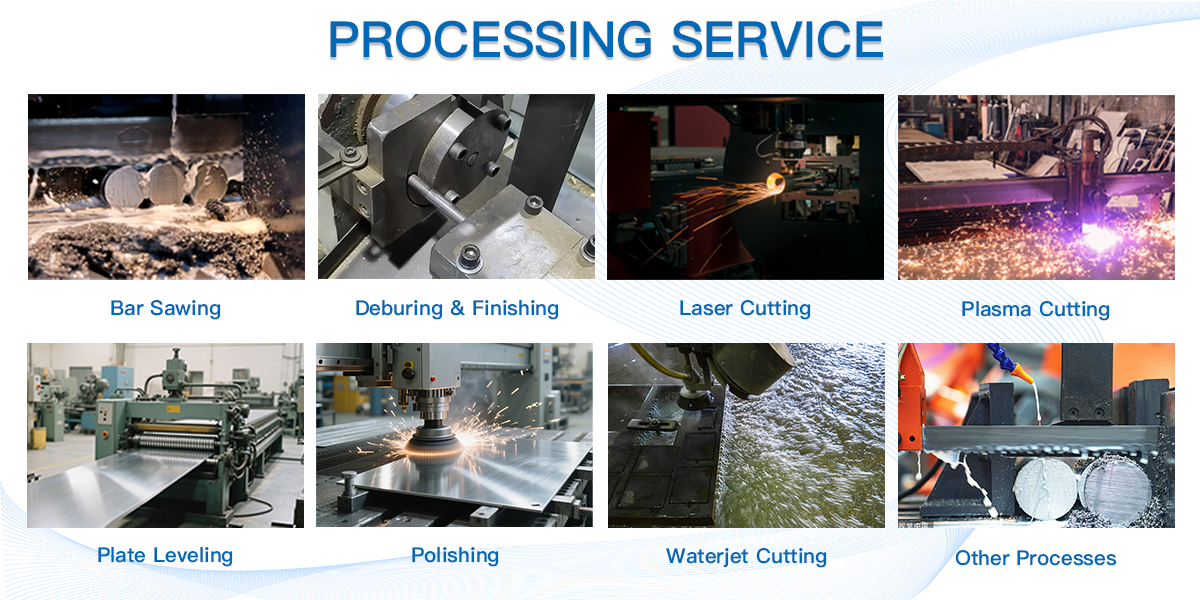
Hot Working: 1176-954°C (2150-1750°F); forging at 1176-968°C (2150-1775°F) . Cold Working: Standard tooling applicable; soft die materials (bronze, zinc alloys) recommended to minimize galling. Heavy-duty lubricants required; all lubricant residues must be thoroughly cleaned after forming to prevent embrittlement . Machining: Work-hardens during cutting; requires heavy-duty equipment, rigid setups, and sharp tools. Water-based coolants for high-speed operations (turning, milling, grinding); heavy lubricants for drilling, tapping, broaching, boring . Welding: Good weldability using GTAW, GMAW, SMAW, and submerged-arc welding. Matching filler metal recommended. Surface must be clean and free from oil, paint, or crayon stains before welding .
Applications Gas turbine hot section components Industrial furnace structural parts Heat treatment equipment High-temperature fasteners and fixtures Power generation system components
Contact ZYTC Alloy for certified Alloy PE11 (UNS N09901 / 2.4662) materials with complete traceability, technical datasheets, and competitive pricing on standard sizes or custom-fabricated components. Email:daisy@zytcsteel.com WhatsApp/WeChat: +86 17335753350 |