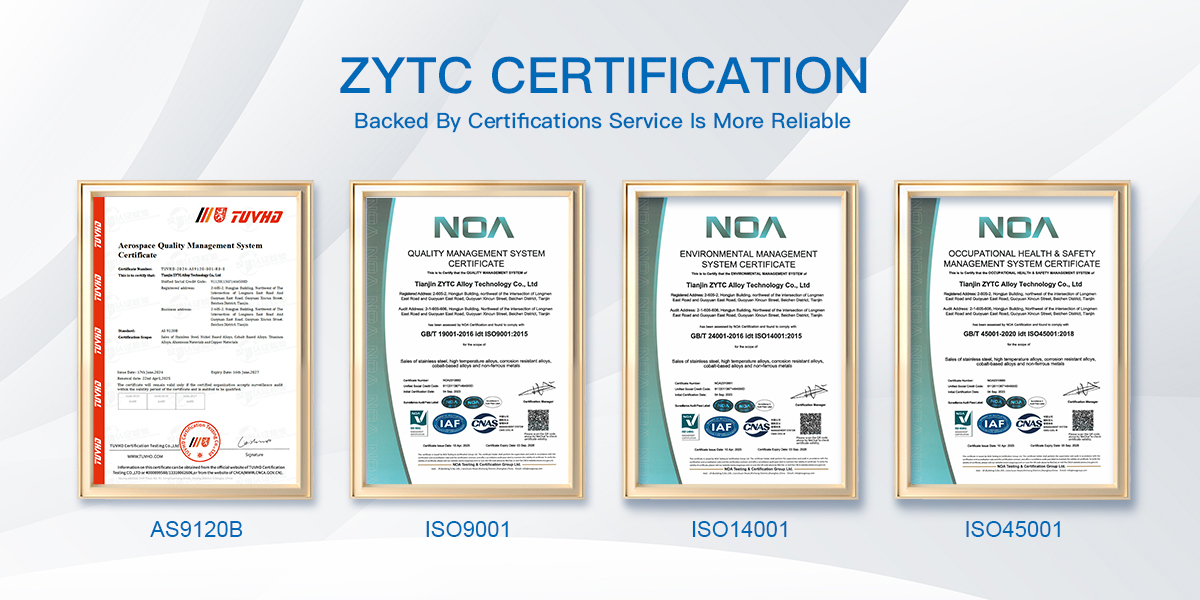
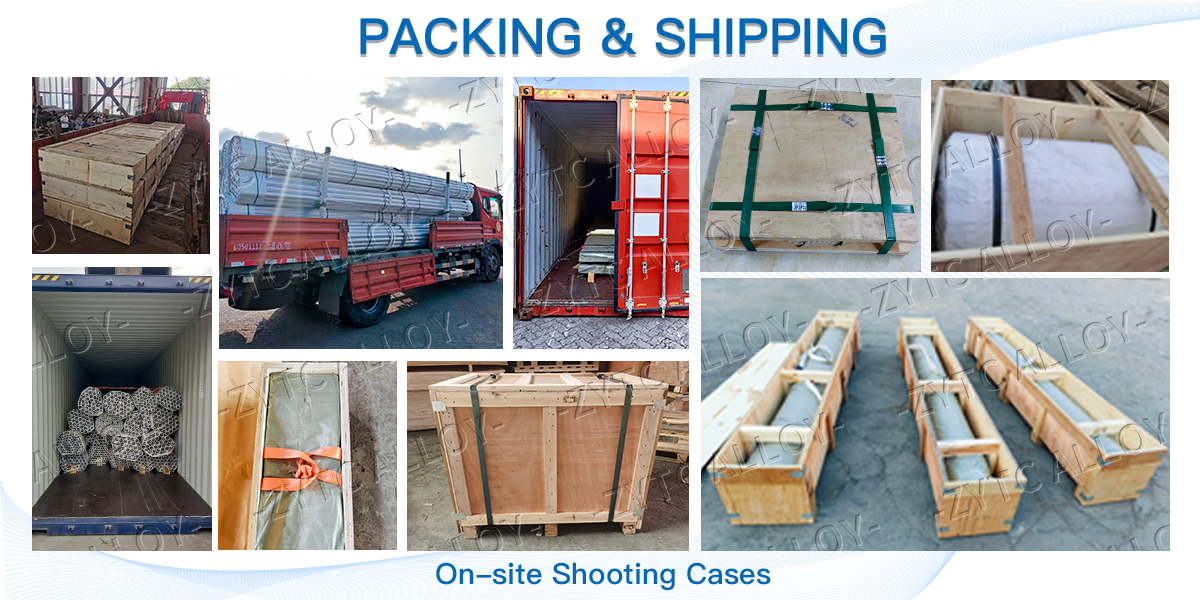
Supply in Cold Worked + Aged condition. Full EN 10204 3.1 MTR with measured chemistry and mechanical properties. Bar, wire, tube, and hollow bar available. Third-party inspection (SGS, BV, TÜV) on request.
Why Source MP35N from ZYTC Alloy① Correct delivery state, documented.
Every batch for sour service is supplied in the Cold Worked + Aged condition required for NACE MR0175 / ISO 15156-3 qualification. The MTR states the aging temperature and time—not just"MP35N." ② Melting route disclosed.
VIM+VAR (vacuum induction melting + vacuum arc remelting) is documented for every heat, minimizing inclusions that can initiate cracking in H₂S environments. ③ Measured data, not pass/fail statements.
Chemistry (Ni, Cr, Mo, C) and mechanical properties (yield strength, tensile strength, hardness) are reported as actual measured values on the MTR. Batch-specific, traceable to the heat number. ④ In-house laboratory verification.
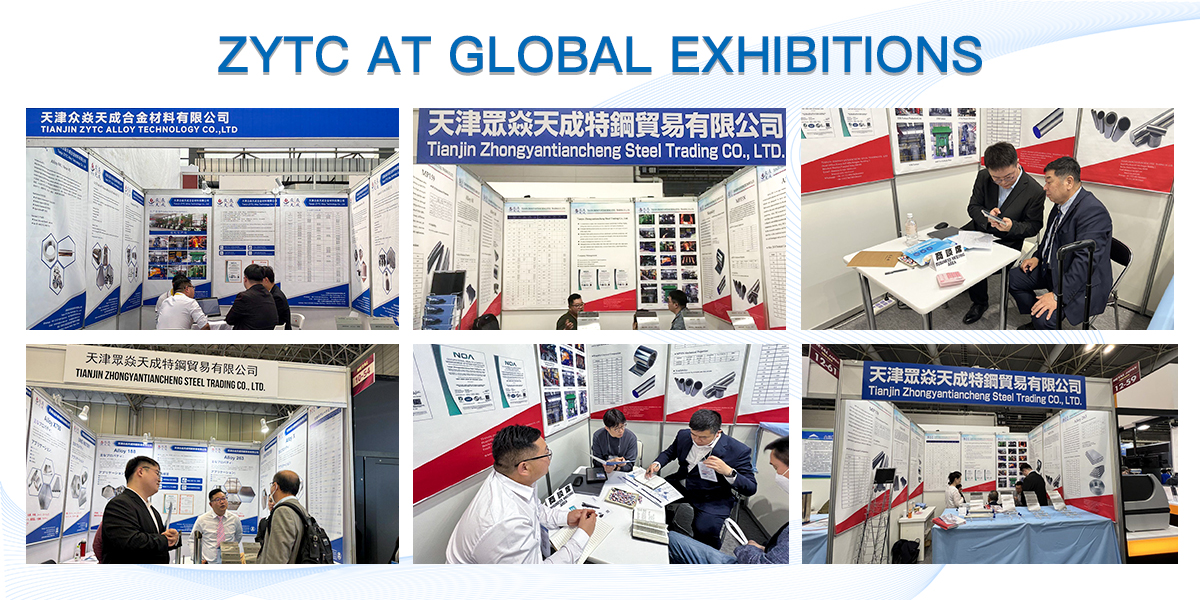
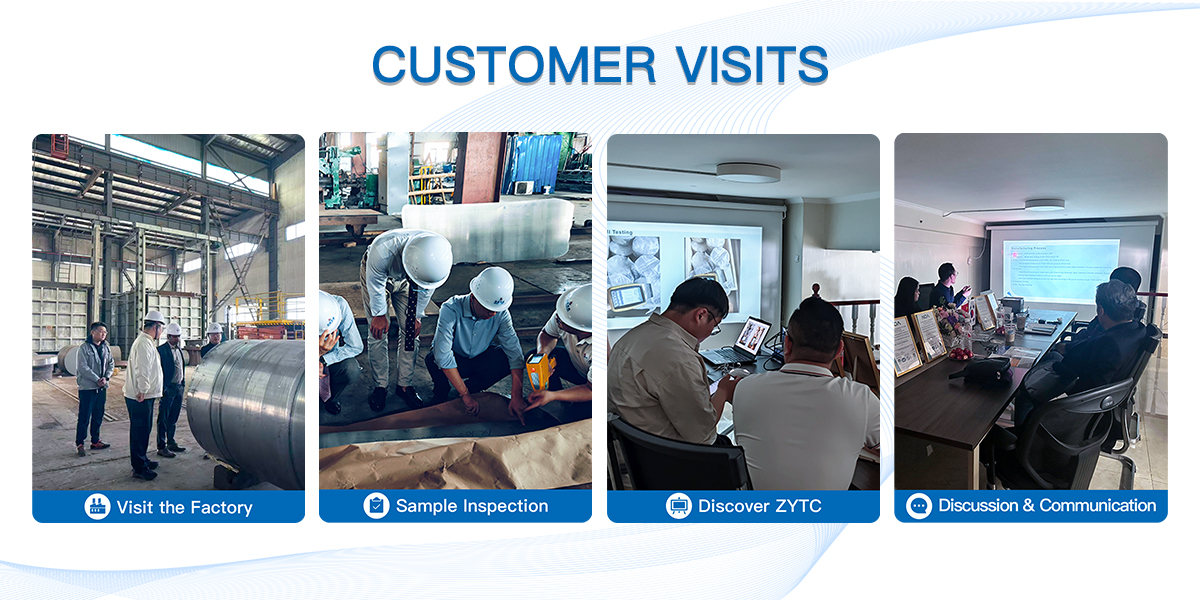
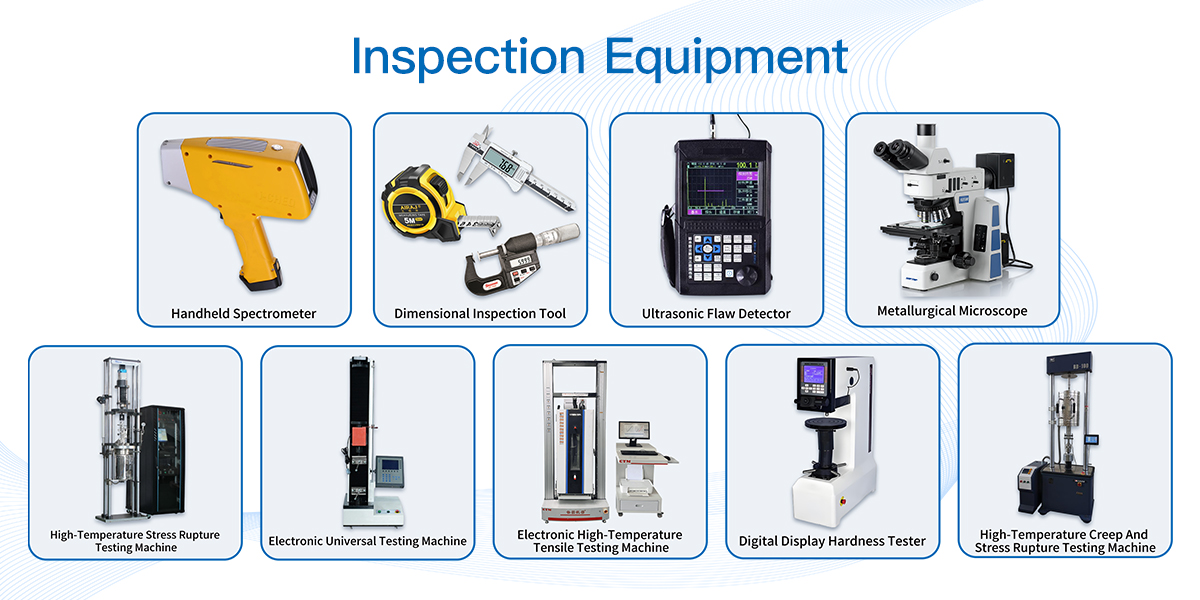
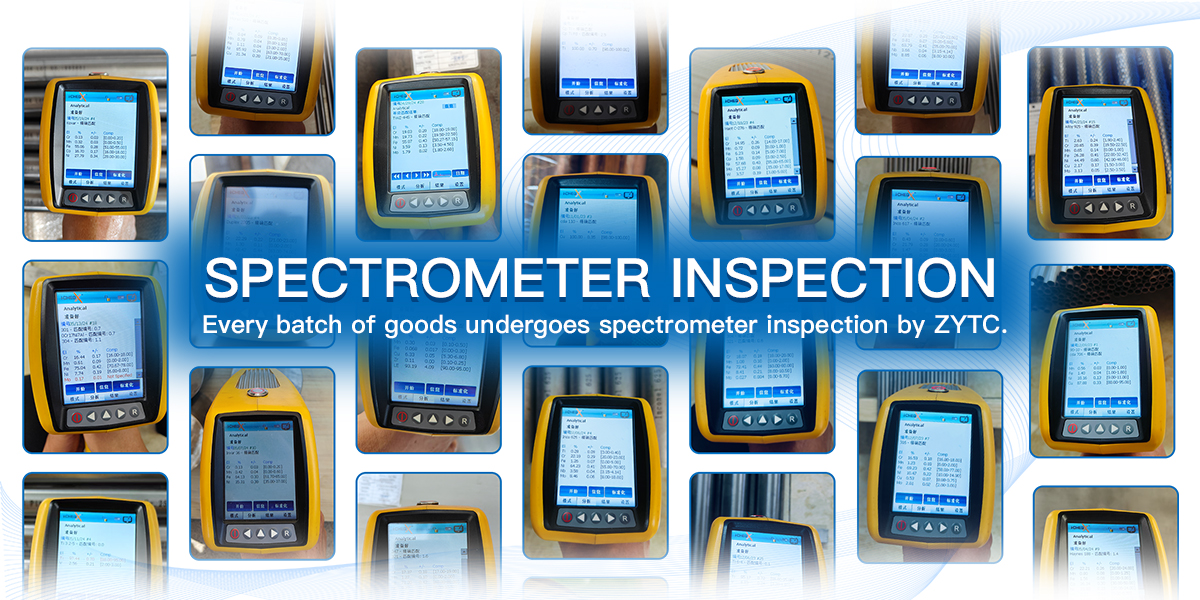
We do not rely on supplier paperwork. Every batch is physically tested in our own lab using spectrometers, universal testing machines, and metallurgical microscopes. Your MTR is backed by real test data. ⑤ Third-party inspection available.
For critical sour service projects, we coordinate SGS, BV, or TÜV inspection upon request.
Available Forms & Typical Sour Service Applications| Form | Typical Application |
|---|
| Round Bar | Downhole tool components, valve stems, completion equipment | | Wire | Wireline, logging cable, slickline, springs | | Tube / Hollow Bar | High-pressure mandrels, polished bore receptacles (PBRs) | | Fasteners | High-strength bolts for wellhead and manifold assemblies |
Size range: Confirm per inquiry. Standard sizes in stock; non-standard sizes quoted on request. |  |
Delivery State & Mechanical PropertiesFor NACE MR0175 / ISO 15156-3 applications, MP35N must be supplied in the Cold Worked + Aged condition. Annealed material does not respond to aging and does not qualify for sour service. The strength you receive depends on cold reduction and aging temperature. Typical values for Cold Worked + Aged MP35N: | Aging Condition | Yield Strength (Rp0.2) | Tensile Strength (Rm) | Hardness (max) |
|---|
| 704°C / 4h | 1448 MPa | 1517 MPa | 51 HRC | | 732°C / 4h | 1379 MPa | 1448 MPa | 51 HRC | | 774°C / 6h | 1241 MPa | 1310 MPa | 51 HRC |
Data source: Sverdrup Steel published NACE MR0175 data for MP35Nbar up to 2 diameter. Actual values depend on cold reduction and product form; ZYTC provides batch-specific test data with every shipment. If your design requires a specific yield strength, state it in the inquiry. The processing window determines the result—do not assume that"MP35N, Cold Worked + Aged"automatically delivers a particular strength level. Hardness note: NACE MR0175 lists MP35N at a maximum hardness of 35 HRC in some conditions, with higher hardness (up to 51 HRC) permitted in specific cold-reduced plus aged conditions. The applicable limit depends on product form and standard edition. Cite the exact edition on your purchase order.
Chemical Composition (ASTM F562 / ISO 15156-3)| Element | Content (%) |
|---|
| Nickel (Ni) | 33.00 – 37.00 | | Chromium (Cr) | 19.00 – 21.00 | | Molybdenum (Mo) | 9.00 – 10.50 | | Carbon (C) | ≤ 0.025 | | Iron (Fe) | ≤ 1.00 | | Titanium (Ti) | ≤ 1.00 | | Manganese (Mn) | ≤ 0.15 | | Silicon (Si) | ≤ 0.15 | | Sulfur (S) | ≤ 0.010 | | Phosphorus (P) | ≤ 0.015 | | Cobalt (Co) | Balance |
Measured values reported on every MTR. Carbon is particularly important—it affects sensitization and weldability.
How ZYTC Verifies Every Batch (In-House Laboratory)To ensure your MP35N meets NACE MR0175 requirements, we do not rely on supplier paperwork alone. Every batch for sour service is physically tested in our in-house laboratory: 📊 Chemistry Verification
Using our Direct Reading SpectrometerandHandheld Spectrometer, we verify Ni, Cr, Mo, and C within ASTM F562 limits, ensuring the alloy will resist SSC in H₂S environments. Measured values are reported on the MTR. 💪 Mechanical & Hardness Testing
OurComputer-Controlled Servo Universal Testing MachineandElectronic High-Temperature Universal Testing Machine confirm the yield and tensile strength. Hardness is strictly measured using our Brinell Hardness Tester to ensure it stays within the safe NACE limit. 🔬 Microstructural Cleanliness
To prevent crack initiation, inclusions must be minimized. We use a Metallurgical Microscope (with Grain Size Analysis) and a Double-Disc Metallographic Polishing Machine to prepare and inspect the microstructure, verifying grain size and cleanliness. 🔨 Impact Toughness
For critical downhole components, our Computer-Controlled Pendulum Impact Testing MachineandImpact Test Notch Projector measure impact energy, ensuring the material is not brittle.  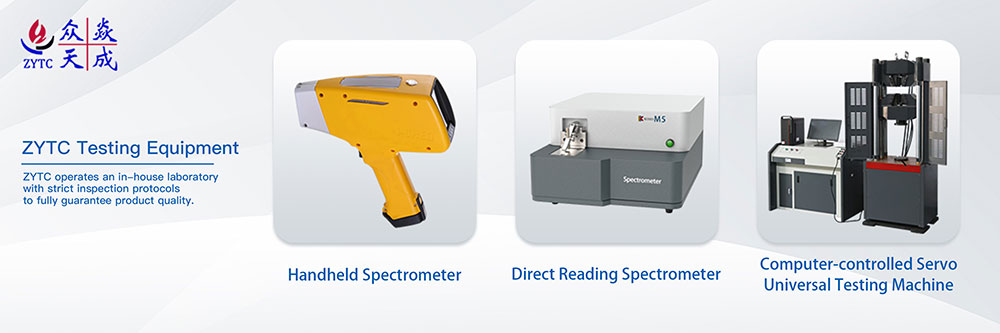 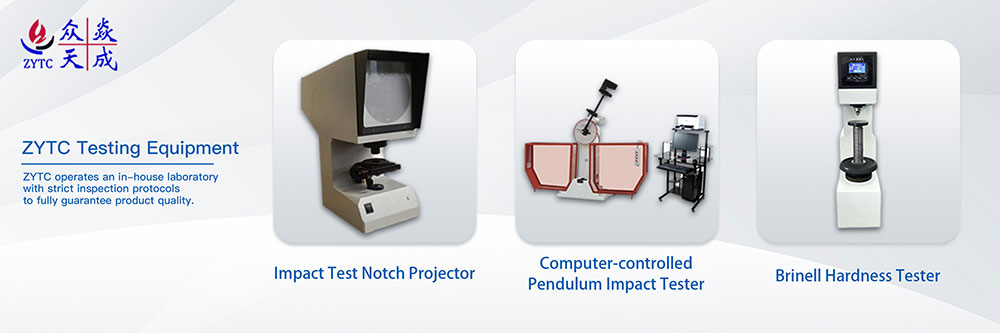
What to Verify on the MTR Before Accepting a ShipmentFor sour service, a supplier's claim of"NACE compliant"is not sufficient. The MTR should show the following: | Item | What"Good"Looks Like | Red Flag |
|---|
| Delivery state | Explicitly states"Cold Worked + Aged"with aging temperature and time | "MP35N"only, or"annealed" | | Melting route | VIM+VAR documented | Undisclosed, or"vacuum melted"without details | | Chemistry | Ni, Cr, Mo, C reported as measured values within limits | "Conforms to ASTM F562"without numbers | | Yield strength | Reported with test method (ASTM E8) and specific value | A range so wide it's meaningless | | Hardness | Reported in HRC with test method (ASTM E18) | Pass/fail only, or no scale stated | | Heat treatment record | Time-temperature curve traceable to heat number | "Heat treated per standard" | | Standard edition | PO and MTR cite ISO 15156-3:2015 (or current edition) | "NACE compliant"without edition |
Request a QuoteTo receive a quotation with full MTR traceability, please provide: Product form and dimensions (bar diameter, wire diameter, tube OD/ID) Required delivery state (Cold Worked + Aged for NACE applications) Target yield strength (if your design requires a specific value) Service environment (H₂S partial pressure, temperature, chloride concentration, pH—if available) Standard edition (e.g., ISO 15156-3:2015) Quantity (kg or meters) Third-party inspection requirement (SGS, BV, TÜV, or none)
If your component involves springs or acid treatment exposure, note this in the inquiry—surface finish and galvanic coupling conditions may affect material performance and should be reviewed before quoting. 📧Email:daisy@zytcsteel.com
📱WhatsApp/WeChat: +86 17335753350 |